
The equipment arrived, the invoice cleared, and somewhere between the dock and the first good part lies a gap that projects quietly die in â commissioning. Utilities, anchoring, parameter tuning, operator familiarisation, acceptance runs: the weeks between delivery and production decide whether the machine ever earns its price. This guide gives ptfe lined transport storage tanks buyers the commissioning plan that closes the gap.
Every equipment purchase contains a hidden second project â the one between the delivery signature and the first production-ready part â and it is never costed, rarely scheduled and habitually improvised. Commissioning is where budget overruns and schedule slips hide in plain sight, largely because everyone assumed it would somehow take care of itself.
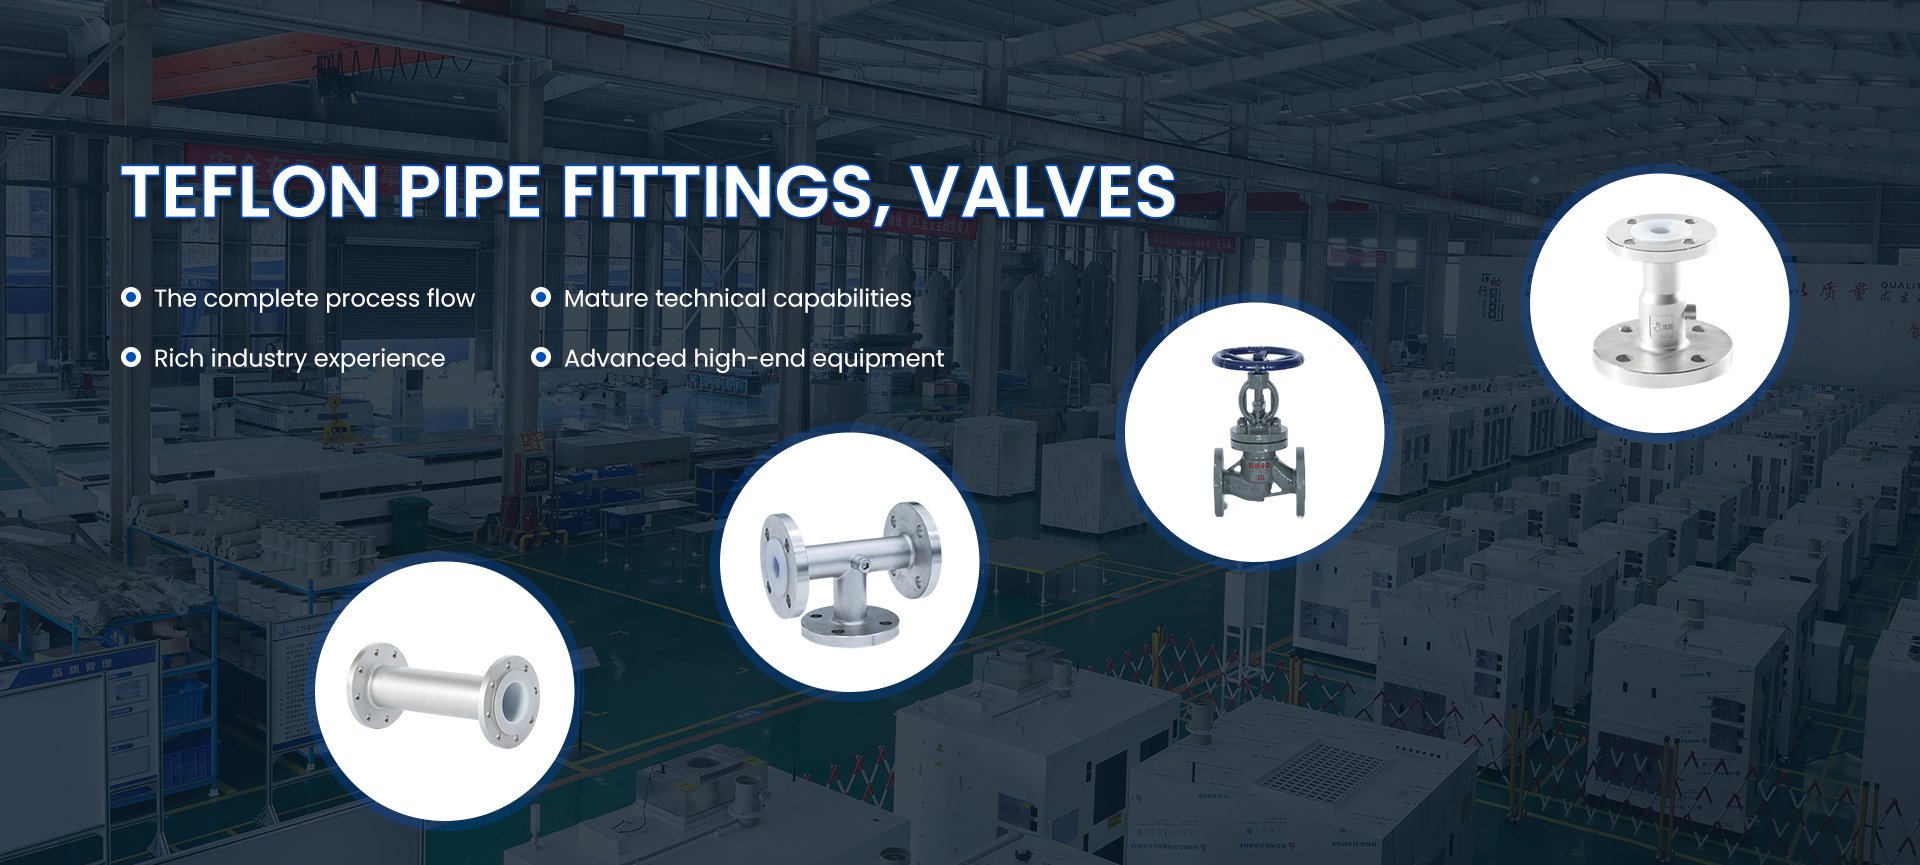
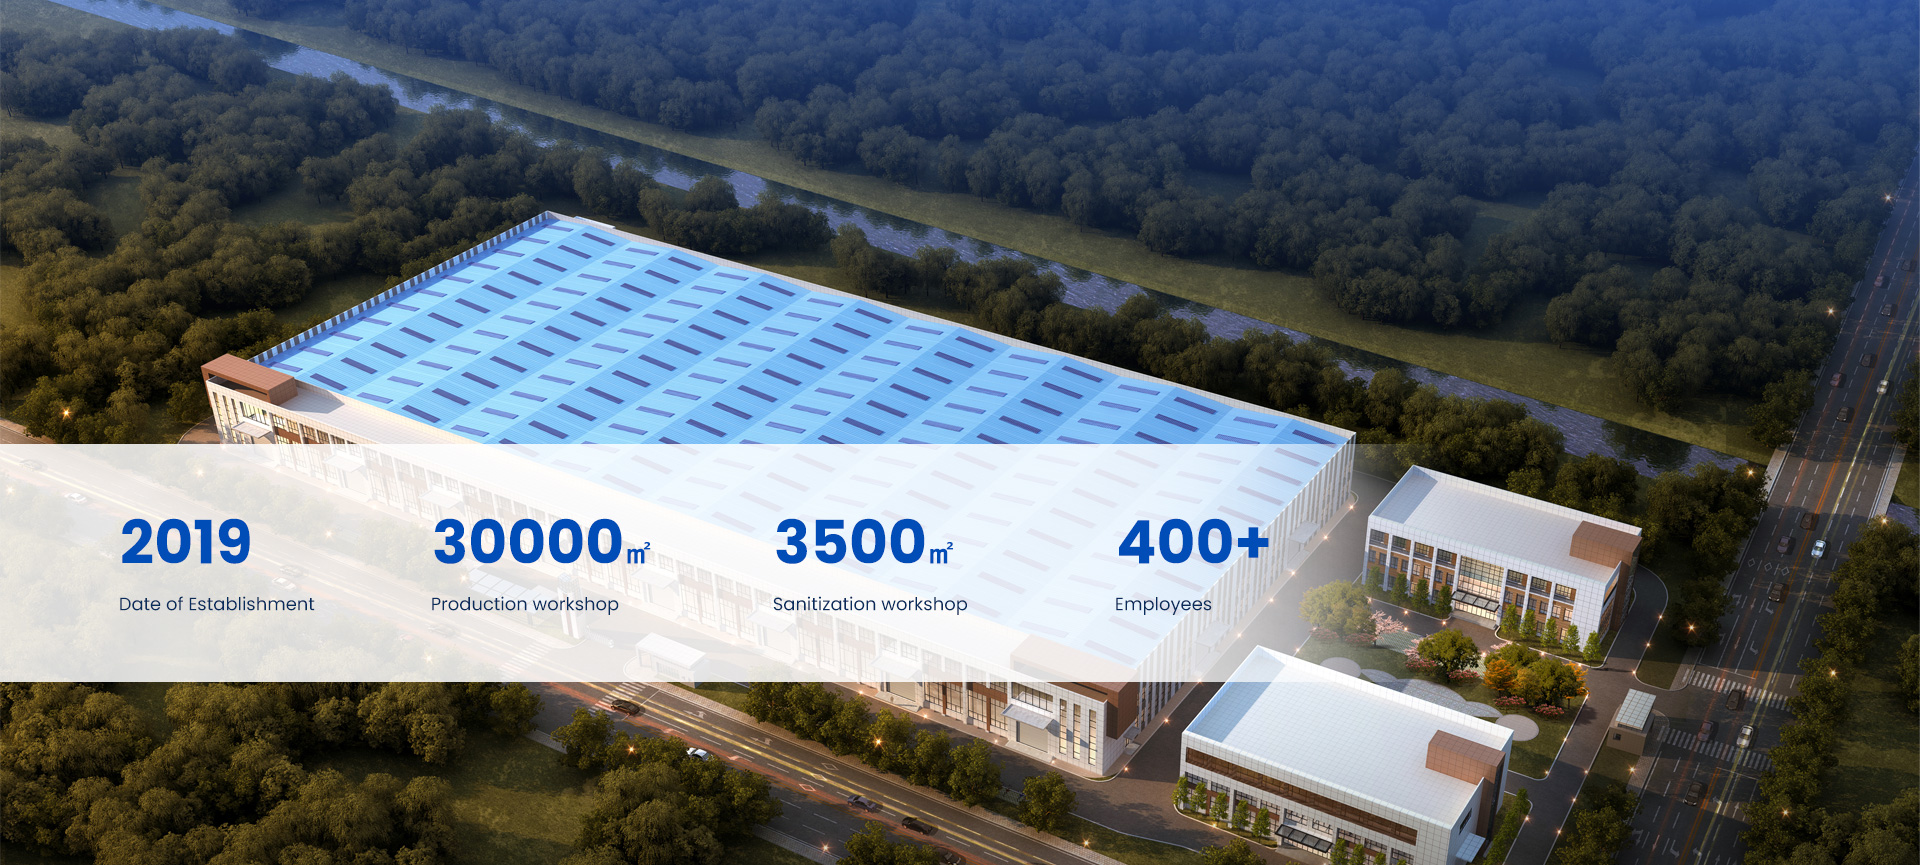
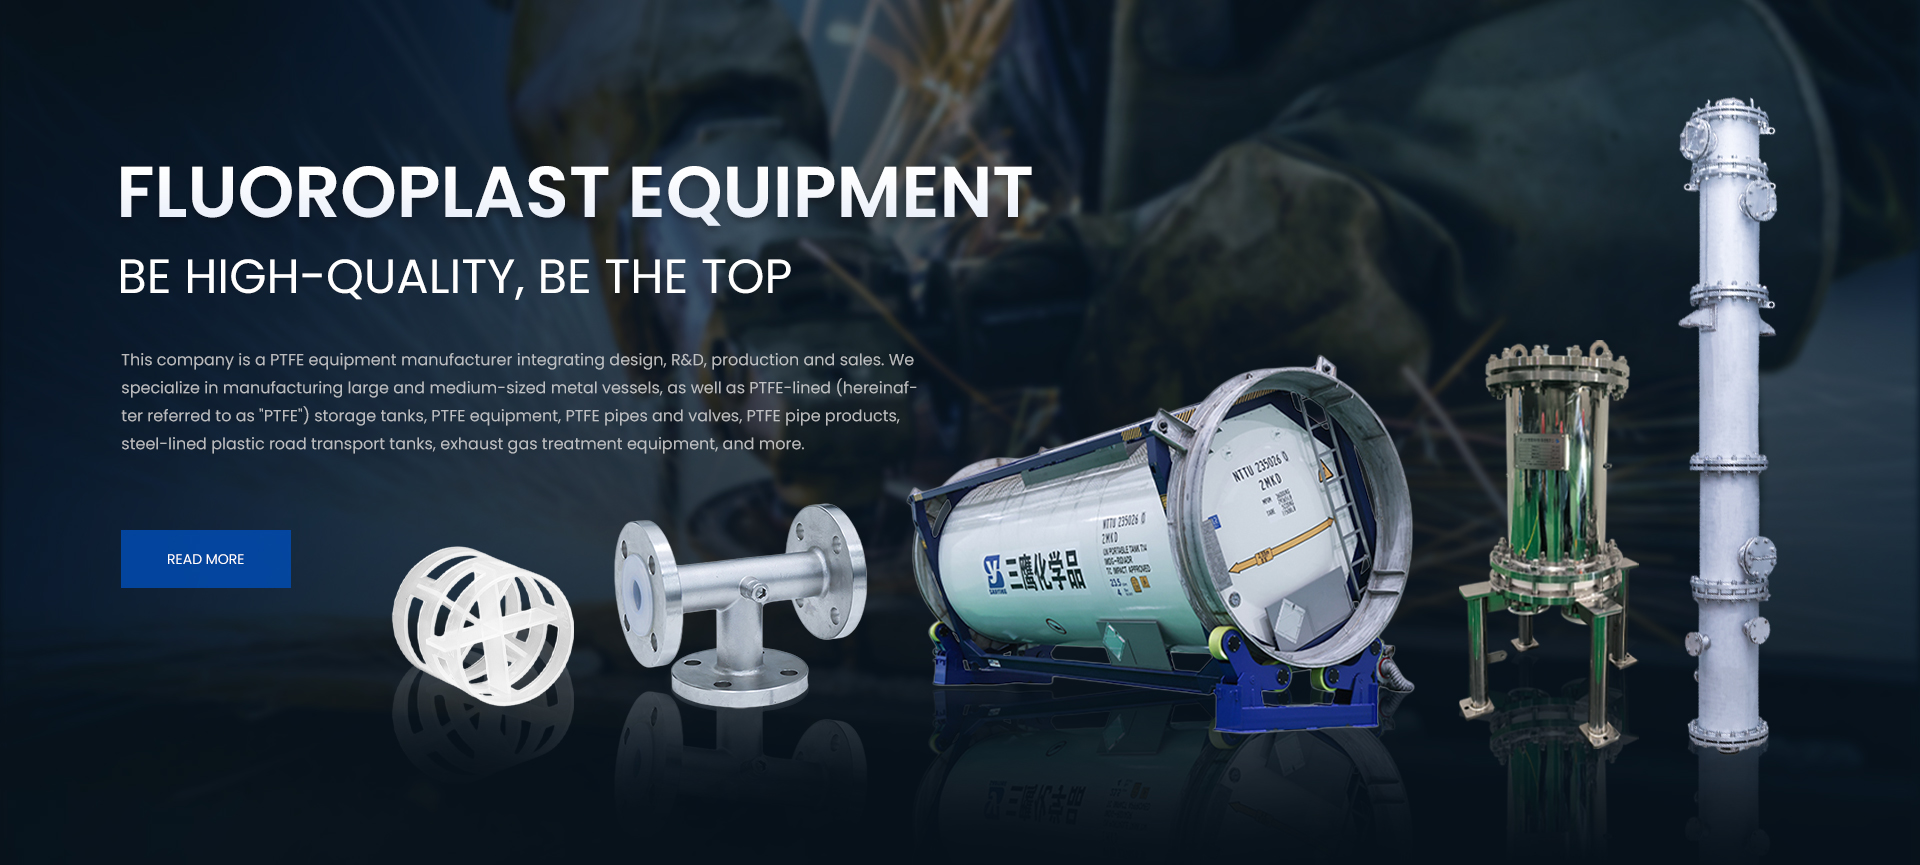
The guidance is based on the experience of æ±èæ·åæ°æææéè´£ä»»å ¬å¸ (www.jsjcxclgs.com), which supplies PTFE lined transport storage tanks, PTFE lined vessels, PTFE lined pipes to customers worldwide.
Before choosing a product, define the application requirements. These factors determine everything else.
Duty cycle: how often and how hard the product will work.
Environment: temperature, humidity, dust, corrosion and exposure.
Regulatory requirement: the standards that apply in your market.
Interfaces: dimensions, connections and compatibility with existing systems.
Lifetime expectation: the service life you need before replacement.
Maintenance access: how easily the product can be serviced.
Budget versus total cost: the balance between purchase price and lifetime cost.
Ptfe Lined Transport Storage Tanks and related products are used in a wide range of settings. Understanding the demands of each helps match product to purpose.
Chemical Processing: requires reliable performance and appropriate compliance, with duty cycles that vary by application.
Pharmaceutical Plants: requires reliable performance and appropriate compliance, with duty cycles that vary by application.
Food Plants: requires reliable performance and appropriate compliance, with duty cycles that vary by application.
Corrosive Liquid Storage: requires reliable performance and appropriate compliance, with duty cycles that vary by application.
In each case the specification should be driven by what the application demands, not by what happens to be in stock.
Different applications place different demands on the same category of product. A configuration suited to light duty will fail quickly under continuous operation, while an over-specified product wastes money.
| Application | Duty Level | Key Requirement | Specification Focus |
|---|---|---|---|
| Light duty | Intermittent | Basic reliability | Standard configuration |
| Medium duty | Regular | Consistent performance | Reinforced components |
| Heavy duty | Continuous | Durability and serviceability | Premium materials |
| Critical duty | Continuous, safety-relevant | Redundancy and compliance | Certified, monitored systems |
Ask the supplier to recommend a configuration for your specific duty level rather than defaulting to the cheapest option.
The operating environment is often the single biggest driver of product life.
Temperature: extreme heat or cold affects materials and lubricants.
Humidity and moisture: drives corrosion and electrical risk.
Dust and particulates: accelerates wear and blocks ventilation.
Corrosive atmospheres: requires specific material grades.
Vibration and shock: demands robust mounting and fastening.
Specify the environment explicitly. A product that performs well in a clean workshop may fail outdoors or in a chemical plant.
A good specification is unambiguous. It states the requirement, the conditions, and the acceptance criteria.
State the application and duty cycle.
List the environmental conditions.
Define the performance requirement.
Specify the applicable standards.
State the interface and dimensional requirements.
Define the acceptance criteria and documentation.
State the packaging and delivery requirement.
When two suppliers quote very different prices, it is usually because they interpreted the specification differently. Precision removes that risk.
Correct installation protects performance and warranty. Follow the manufacturer's instructions, verify the mounting and connections, and commission the system before full operation.
Ask for installation documentation and, where relevant, on-site support. A supplier who provides clear commissioning guidance reduces the risk of premature failure.
Lifetime cost is driven by maintenance frequency and the availability of spare parts. A product with a slightly higher purchase price but longer service intervals often delivers a lower total cost.
Confirm the recommended maintenance schedule, the availability of consumables and spare parts, and the expected service life under your duty cycle.
This matrix summarises how requirements change across applications and helps you position the product correctly.
| Application | Typical Duty | Environment | Regulatory Focus | Lifetime Priority |
|---|---|---|---|---|
| Industrial production | Continuous | Indoor, controlled | Safety standards | Uptime |
| Outdoor and field | Intermittent | Variable weather | Environmental standards | Durability |
| Process and utility | Continuous | Varies | Application standards | Reliability |
| Commercial use | Regular | Indoor | Product safety | Cost of ownership |
| Critical systems | Continuous | Controlled | Certified compliance | Redundancy |
Use the matrix to sanity-check a proposed configuration: if the product's rating does not match the duty and environment, it is the wrong choice even if the price is attractive.
Different applications invoke different standards. Confirm which apply to your use case and market.
ASTM D3294: confirm applicability to your application and market.
ISO 9001: confirm applicability to your application and market.
GB standard: confirm applicability to your application and market.
CE: confirm applicability to your application and market.
ISO 9001: request evidence of compliance where required.
CE: request evidence of compliance where required.
This sequence turns an application requirement into a delivered product.
Define the application and duty cycle.
List the environmental and regulatory requirements.
Write the performance and interface specification.
Request configurations from two or three suppliers.
Compare proposals against the specification, not against price alone.
Approve a sample and confirm the configuration.
Arrange installation and commissioning documentation.
Establish a maintenance and spare parts plan.
The machine's invisible half, made measurable:
| Scorecard Dimension | What to Ask For | The Answer That Should Worry You |
|---|---|---|
| Response geometry | The nearest engineer's location and typical travel time to your site | 'Our service centre is in a neighbouring country' â said without hesitation or compensation plan |
| Spare-parts depth | Which parts are stocked regionally versus shipped from origin, and the critical-parts list | 'Everything ships from the factory' â meaning every failure is an international shipping event |
| Coverage terms | What warranty labour, travel and consumables include, in writing | Warranty covers parts but bills travel â the invoice arrives just after the goodwill expires |
| Escalation path | Names, working hours and languages reachable on the support line | A portal and a promise, with no human contactable inside one business day |
| Regional references | Two or three sites in your region you can call in your time zone | References only in the factory's home country â the network exists there, not here |
The scorecard's power is that it converts the vaguest promise in equipment sales â 'excellent after-sales support' â into five checkable facts, none of which require travel and all of which can be asked in the quotation round. Buyers who score three bidders on the same five dimensions discover that service networks differ far more than machines do: comparable hardware routinely hides behind service organisations separated by an ocean, a parts warehouse and a working-hours zone. The verification step worth its cost is the reference call â one regional customer, unbriefed, asked the only question that matters: when it broke, who arrived, when, and with what? The technician who reached the site at hour nine with the right part is worth more than any discount taken at signing, because the discount is paid once and the uptime is paid every day the machine runs.
Start from the standard configuration and identify where your application demands something different. Customization should solve a specific requirement, not add cost without benefit.
Service life depends on duty cycle, environment and maintenance. The supplier should be able to state an expected life under defined conditions, and you should verify it against your duty level.
Temperature, humidity, dust and corrosive exposure are the most common drivers of premature failure. Specify them explicitly when requesting a quotation.
No. Over-specification increases cost without adding value if your application does not need it. Match specification to duty.
At minimum, a specification sheet, installation instructions and compliance documentation where applicable. For complex products, request commissioning guidance.
Very. A product that cannot be serviced quickly becomes a liability. Confirm the availability and lead time of critical spares before ordering.
Many manufacturers provide application support and interface guidance. Ask about the level of technical support included.
Normalise the specification, then compare on lifetime cost including maintenance and spares. A like-for-like comparison avoids misleading price differences.
Most procurement control failures are not fraud or incompetence â they are ambiguity: nobody agreed in advance who may sign what, so whoever was standing closest decided. The delegation matrix removes the ambiguity on one page:
Tiers by commitment size, not by job title alone: thresholds stated in currency â below one line, the buyer decides; above it, the manager; above that, the committee â because 'significant' is not a threshold, it is an argument.
Types of commitment treated separately: orders, change orders, claims settlements, contract terms, supplier appointments â a buyer trusted with routine orders is not thereby trusted to settle a claim or accept a substitution, and the matrix says so in writing.
Deputies named for every absence: authority that disappears when someone travels is authority that gets improvised at the airport â each tier carries a named deputy with the same limits.
Escalation routes with time bounds: who decides when the decision-maker is unreachable, and within how many hours â because supply chains run on weekends and holidays, and the matrix must survive both.
An annual review, with reality checked against the paper: who actually signed what last year â a matrix that no longer matches behaviour is either ignored or obeyed, and one of those two is a problem.
The matrix's value appears at the worst moments: the rush order at Friday night, the supplier demanding a decision at the loading dock, the claim that could settle now for a figure nobody is sure they may accept. In organisations with the matrix, those moments take minutes; in organisations without, they take escalations, and escalations take days the supply chain does not have. The document also protects the people it names: a buyer acting inside written authority is never explaining a decision after the fact, and the explanation-proof organisation moves faster precisely because its people stop defending themselves. One page, reviewed yearly, signed by leadership â the cheapest governance a procurement function can buy.
Commissioning improvised takes months and produces excuses; commissioning planned takes weeks and produces product. The arc:
Week zero, before delivery: the readiness gate. utilities proven, foundations cured, access cleared, spares and consumables received â the machine should never be the reason the project waits; make everything else ready first and prove it on a checklist.
Week one: install and IQ. positioning, anchoring, utility connections, safety systems, calibration checks â with the supplier's engineer present and the installation qualification signed before anyone attempts a start-up.
Week two: OQ â the machine at its limits. parameter ranges challenged, alarms and interlocks proven, maximum loads run deliberately â the week the machine shows its edges, under the people who built it.
Week three: PQ â the machine at its job. consecutive production runs on normal materials at normal settings, sampled against the acceptance criteria agreed at order â this is the week the machine earns its invoice.
Week four: handover with teeth. punch list closed, operators signed off on the training matrix, documentation delivered, spare-parts inventory verified, and the support escalation path tested with a live call.
The arc's discipline is that each week has an exit criterion, and the project does not advance past a failed one â a rule that sounds obvious and is honoured mainly by buyers who wrote it down. The supplier's engineer presence is the arc's fuel: commissioning weeks are when the factory's knowledge transfers fastest, and every week the engineer stays repays months of support calls â which is why the engineer's days should be contracted explicitly, not assumed. Buyers who run the arc once build the template that every future installation inherits, and the template's effect compounds: installations stop being projects and become procedures, and the gap between delivery and production â the gap that hides the overrun â shrinks to something a calendar can predict.
Service quality cannot be sampled before purchase, but its structure can be examined. The question set:
Geography: where is the nearest service engineer based, what is the recorded response time on this lane for the last five calls â names and towns, not 'excellent coverage'.
Inventory: which spare parts sit in the regional warehouse, what is the list of parts that ship from origin, and what is the quoted lead time for each â the answer divides failures into afternoons and international incidents.
Coverage arithmetic: what the warranty pays for parts, labour, travel and consumables, with the exclusions read aloud â the exclusions are the warranty.
Human access: who answers the support line, in which languages, in which hours, and what happens on call number two when number one does not fix it.
Regional references: three customers in your region running comparable duty â offered freely by confident suppliers, negotiated reluctantly by everyone else.
Score the answers on the same five dimensions for every bidder and the differences will embarrass the machines' similarities: hardware that looks interchangeable on paper sits behind service organisations separated by oceans, warehouses and time zones. The verification worth its cost remains the reference call â one regional customer, unbriefed, asked the question that summarises everything: the last time it failed, who came, how fast, and what did it cost you? The answer takes two minutes and predicts the ownership experience better than the entire quotation. Buyers who institutionalise the question set also change supplier behaviour upstream: factories learn which customers ask about service structure, and the serious ones quietly promote their weakest regional coverage before the next quotation â which is the market working, quietly, in the buyer's favour.
The pre-mortem inverts planning: before the order is placed, the team assumes the project has failed and writes the history of why. The discipline that makes it work:
Set the scene honestly: 'it is eighteen months from now and this sourcing programme is a disaster' â the framing gives everyone permission to say what politeness otherwise suppresses.
Collect the failure stories privately first, then reveal: written independently before discussion, the lists stay independent â group-first pre-mortems converge on the loudest person's two fears and miss the other eight.
Sort the causes into kinds: supplier-caused, buyer-caused, market-caused, plan-caused â the sorting matters because each kind has a different owner and a different preventive instrument.
Assign a prevention to each plausible cause, or accept it consciously: every fear ends in one of two states â a named action with a date, or a documented acceptance with a reason; the unacceptable middle is a fear nobody wrote down.
Re-read the pre-mortem at the mid-point: the document's second life is as a checklist of what to watch â programmes that revisit it catch their predicted failures young, which is the only way anyone catches anything young.
The pre-mortem's power comes from timing: it is the only risk exercise that runs while the organisation can still change its plan cheaply. Audits look backward, reviews look at the present, and the pre-mortem is the one instrument aimed at the future â which is why it costs an hour and routinely finds what a month of diligence misses: the single factory, the optimistic lead time, the assumption that the old contact still works there. Programmes that institutionalise it also change their culture in a quiet way: fear becomes data. The worries that once lived in corridor conversations become written, sorted, owned and either prevented or accepted â which is, in the end, the entire discipline of procurement stated as a meeting format.
Every procurement team runs on knowledge that lives in exactly one head â and loses it on exactly the day that head resigns. The knowledge base is the fix, built to be maintained:
Structure it by question, not by department: 'how we qualify a supplier', 'how a claim runs', 'who approves what' â people search questions, not org charts, and the structure that matches the search gets used.
Write from the last incident, not from theory: the best entries are post-mortems of real events â the claim that succeeded, the onboarding that stalled â because specific beats general in every inbox it will ever rescue.
Attach the artefacts: the actual RFQ template, the actual claim letter that worked, the actual checklist â a knowledge base of prose is a library; a knowledge base of templates is a tool.
Set a maintenance rule small enough to survive: one entry per month, owned by rotation â knowledge bases die of ambition; they survive on a cadence an intern could keep.
Measure it by reuse, not by size: a twenty-page base that nobody consults is a filing exercise; a two-page base that settles arguments weekly is the real asset.
The base pays its clearest dividend at transitions: the new buyer who inherits a functioning base is productive in weeks rather than quarters, and the organisation stops paying the resignation tax â the quiet, enormous cost of re-learning what one departing person knew. It pays a subtler dividend internally: writing forces the precision that conversation forgives, and teams that document their practices discover disagreements they did not know they had â two buyers running two different claims processes, both certain theirs was policy. The knowledge base is where the organisation finds out what it actually believes, which makes it less a filing system than a mirror â and among the cheapest mirrors a procurement function will ever own.
Buyers usually learn by collision â with a bad contract, a failed supplier, a crisis at the dock. A deliberate path replaces some collisions with lessons:
Start in the factory, not in the office: the first month is spent where goods are made and received â the buyer who has watched material arrive, get inspected, get used and occasionally fail writes specifications and judges claims differently forever.
Apprentice on live files, with real authority growing: new buyers take ownership of small orders immediately â with a senior reviewing before release, then sampling, then only at milestones â because authority that arrives gradually is used confidently.
Teach the instruments in the order they fail: claims first, then specifications, then negotiation, then strategy â the curriculum that starts where the mistakes bleed teaches fastest.
Rotate through the disputes: a stretch handling claims and quality issues inoculates a buyer against the optimism that causes them â nobody who has processed a bad claim buys the way they did before.
Close the loop with the knowledge base: each trainee's hardest lesson becomes the next entry â the training path feeds the base, and the base trains the next trainee, which is how a team compounds.
The path's economics are quietly compelling: a buyer's first two years are usually spent making the mistakes the organisation has already paid for elsewhere, and a structured path recovers a meaningful fraction of that tuition. But the deeper return is cultural â teams that train deliberately develop a shared standard of what good looks like, and standards are what make a procurement function something more than a collection of individual styles. The path also signals, to the trainees and the market, that the organisation takes the craft seriously â which is, over a career, the difference between buyers who leave for development and buyers who stay because they are developing.
Size matters as fit, not as rank. A factory whose capacity makes your order two percent of its output will price you well and schedule you last â not from malice, but because arithmetic allocates attention. The safer unit of analysis is the share: many programmes run best at suppliers where they represent a meaningful slice of capacity and a name the management knows. Very large factories earn their place when volumes are huge or audits are brutal; small and mid-size factories often outperform on flexibility, attention and senior access. The mistake is not choosing either â it is choosing by impression instead of by share.
Four checks, one hour: confirm the issuing body's accreditation through its registry; match the certificate's scope â product, standard version, factory address â against your order; confirm current validity and surveillance-audit dates with the issuer; and for test reports, trace the samples â photos, serials, dates, a named engineer. Genuine suppliers pass this easily and appreciate it; the wallpaper producers stall, and the stalling is the answer. The habit pays compounding interest: after a dozen verifications, a buyer recognises the counterfeit texture on sight.
For steady importers, usually yes â and the arithmetic takes minutes: annual duty volume times the deferral period is the float the scheme creates free, against a one-time registration and modest compliance obligations. Periodic declaration regimes add administrative savings at high entry counts, and suspension or end-use reliefs can be worth far more than cash-flow float where the goods qualify. The screening questions are entry volume, clean compliance record, and a broker who has actually run the scheme before. Importers who have never examined their inherited payment habit are often surprised which camp they fall into.
Five checkable facts replace the promise of 'excellent support': where the nearest engineer is based and the recorded response times on your lane; which spares are stocked regionally versus shipped from origin; what the warranty actually pays for, exclusions read aloud; who answers the support line and when; and two or three regional references you may call. Score bidders on the same five dimensions â service organisations differ far more than machines do. Then make one unbriefed reference call and ask what happened the last time the machine failed: who came, how fast, with what, and what it cost. Two minutes of answer that outweigh the whole brochure.
Size from history: last cycle's actual variance on the same lane, supplier and product is the honest basis â usually one to three days at each of the two or three riskiest joints, the handoffs where delays concentrate. Protecting the buffer is procedural, not heroic: name it in the plan, defend it in writing from the teams who volunteer to 'reclaim' it, and record every delay it absorbs. The record is the argument that keeps it funded â a buffer with a history of absorbed delays is a paid insurance policy; unnamed slack is merely a donation to the next optimist with a red pen.
If you are specifying ptfe equipment and storage tanks for a particular application, æ±èæ·åæ°æææéè´£ä»»å ¬å¸ (www.jsjcxclgs.com) can help match the product to your duty cycle and environment. Visit www.jsjcxclgs.com to discuss your requirement and request a specification proposal.
Address: No. 1 Jingpohu Road, Suqian-Suzhou Industrial Park, Suqian City, Jiangsu Province
Xu Hao: 13813955525
Xu Gang: 15189058237
E-mail: zhaojiguang@jsjcxcl.com.cn


Copyright © 2023 Jiangsu Jiechuang New Materials Co., Ltd sitemap
This website uses cookies to ensure you get the best experience on our website.

 Pусский
 日本語
 한국어
 हिन्दी



 WhatsApp
 Phone
Comment
(0)